Specifying laser surface preparation
Which documents apply to laser-prepared steel, how to state cleanliness and profile in a specification, and which tests verify the result.
- AMPP documents
- SP21511-1 and Guide 21611, both 2024
- Their scope
- Pulsed laser ablation
- Profile
- Measured separately from cleanliness
- Governs acceptance
- Your coating data sheet and specification
Standards that apply
AMPP has published a standard and a technical guide for laser ablation of ferrous metals. Both cover pulsed lasers. Extrinite's 2,000 W and 3,000 W rental systems are continuous wave, which both documents place outside their scope.
About these documents
The AMPP documents are purchased, licensed publications. This page names them and summarizes their scope; it does not reproduce them.
AMPP SP21511-1-2024
Laser Ablation for Surface Preparation of Ferrous Metals, Pulsed Laser. Approved August 1, 2024.
Written so specifiers can set surface preparation and cleanliness requirements for pulsed (Q-switched) laser ablation. Continuous wave lasers and ultra-short pulsed lasers are excluded from its scope.
It defines five end states for pulsed laser surfaces: thorough ablation (PLA-TA), partial ablation (PLA-PA), spot and sweep ablation (PLA-SSA), sweep ablation (PLA-SA) and ablation cleaning (PLA-AC). Acceptable cleanliness for recoating is set by the technical authority or the project specification.
AMPP Guide 21611-2024
Pulsed Laser Ablation Technical Guide for Ferrous Metal Substrates. Approved August 1, 2024.
A technical guide to the capabilities and limitations of pulsed laser ablation, written to support SP21511-1. Continuous wave lasers are outside its scope.
It states that pulsed-laser-prepared surfaces are not to be compared with surfaces cleaned by abrasive blasting, and it covers laser controlled areas and laser eye protection to ANSI Z136.1.
SSPC-SP 10 / NACE No. 2
Near-White Metal Blast Cleaning, a cleanliness standard written for abrasive blast cleaning.
Extrinite's equipment data sheets cite "SP-10 / 1–2.5 mils" for rusted surfaces, and Extrinite supports that SP-10 reference for laser-prepared surfaces. The figure combines a cleanliness standard with a profile range, so specify and measure the two separately.
Your coating product data sheet
The document that usually decides acceptance.
Sherwin-Williams Protective & Marine has stated in writing that it approves laser preparation where the surface profile required by the product data sheet for each product is met.
Product data sheets also set recoat limits. Carboguard 890, for example, has a 90-day recoat time; after 90 days the surface must be abraded before more coats are applied.
Cleanliness and profile
A coating specification states a cleanliness requirement and a surface profile requirement. They are separate acceptance criteria and they are measured separately.
One method, several end states
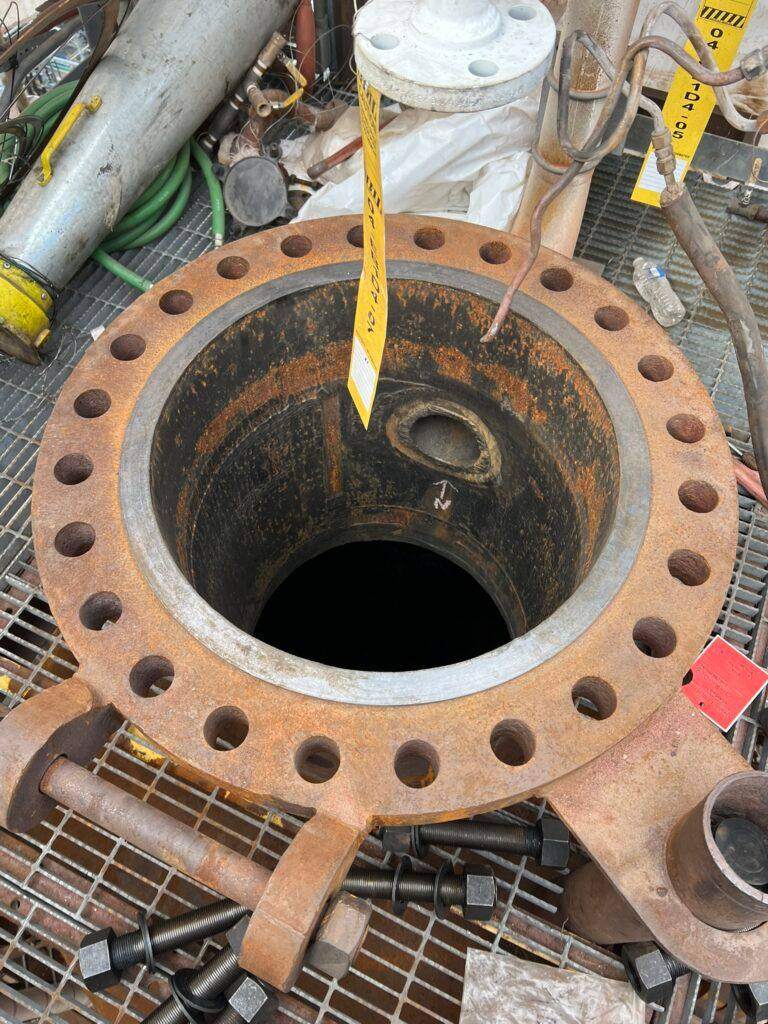
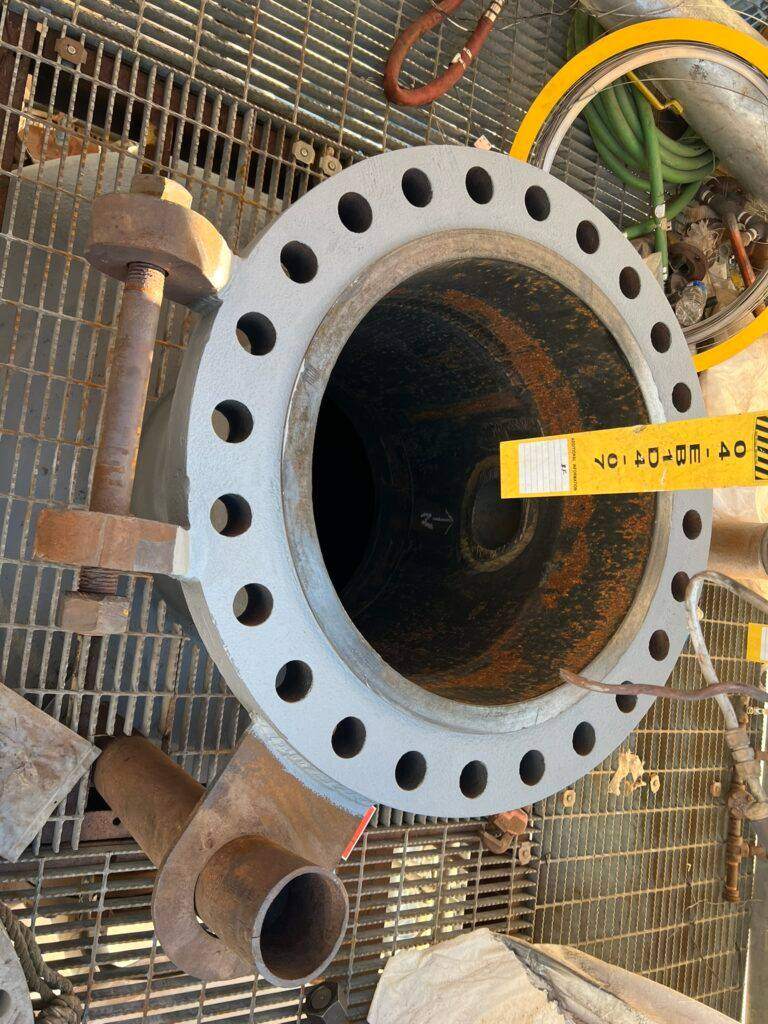
The finished condition depends on the parameters the operator sets and on what the specification asks for. In the Carboguard 890 parameter study, four settings on the same 4–6 mil coating gave four results: coating roughened and retained, most of the coating removed, coating fully removed with the profile still visible, and an intact profile with heat discoloration. On the refinery project the case study records white metal on completion. Write the end state your coating needs into the specification.
- Anchor profile on rusted surfaces, Extrinite operations guidance
- 1–2.5mils
- Measured in coating-removal testing once bare substrate was reached
- 2.5–3.5mils
- Recorded in the Carboguard 890 trial on steel with no previous profile
- 1.98–3.5mils
Extrinite publishes 1–2.5 mils as its anchor profile on rusted surfaces. The other two ranges are measurements from particular tests.
Writing the specification
Six items make a laser preparation scope inspectable. Agree them with the coating manufacturer and the inspector before work starts.
- 01
Name the coating product
Its product data sheet sets the profile and surface condition the coating needs. - 02
State the cleanliness end state
Say in words what the surface must look like and how the inspector will judge it, for example coating roughened and retained, or removed to bare metal. - 03
State the profile and its method
Give the profile range from the data sheet and the measurement method, such as ASTM D4417. - 04
Set the soluble salt check
Laser ablation helps remove surface chlorides. Verify salt levels with the project-specified method, such as Bresle. Flash rust and salts - 05
Require a test patch
A calibration test patch on the actual substrate and coating, with the settings recorded before production work. - 06
Ask for records
Production rate, pass counts, final profile and the parameters used, plus adhesion testing where a coating follows.
Testing and verification
The checks below are named in Extrinite's data sheets, test reports and test planning, or in the AMPP standard. Your specification decides which apply.
| Check | Method | Where it comes from |
|---|---|---|
| Surface profile | ASTM D4417 | Profiles of 1.98, 2.80 and 3.5 mils were recorded in the Carboguard 890 trial |
| Soluble salts (chlorides) | Bresle method; ISO 8502-6 and ISO 8502-9 | Named on the Extrinite data sheets and in Extrinite's test planning |
| Adhesion of the new coating | Pull-off adhesion testing | In the Carboguard 890 trial every pull reached the 3000 PSI gauge maximum, including the untouched baseline |
| Retained coating, where coating is left in place | ASTM D6677 or ASTM D3359 | Cited in AMPP SP21511-1 as tests a specifier may require |
| Dust on the prepared surface | ISO 8502-3 (tape method) | Cited in AMPP SP21511-1 |
| Compressed air cleanliness | ASTM D4285 | Cited in AMPP SP21511-1; the rental systems need dry, oil-free compressed air |
Frequently asked questions
For other questions, call 346.217.6583 or email info@extrinite.com.
Do Extrinite's rental systems conform to AMPP SP21511-1?
SP21511-1 covers pulsed laser ablation, and its scope excludes continuous wave lasers. The 2,000 W and 3,000 W rental systems are continuous wave, so the standard does not apply to them. Specify the surface by its end state, its profile and the tests that verify them.
Can I call up SSPC-SP 10 for a laser-prepared surface?
Yes. Extrinite's data sheets cite SP 10 for laser-prepared surfaces. SP 10 is written for abrasive blast cleaning, so agree with your coating manufacturer and inspector how cleanliness will be judged, and state the profile requirement separately.
Does laser cleaning remove soluble salts?
It helps remove surface chlorides, and on Extrinite's refinery and coating projects hydrocarbons and chlorides came off with the oxidation or coating. Salt levels still need to be verified with the project-specified test before coating.
Is there a longer recoat window after laser cleaning?
Extrinite does not claim one. Coat within the window set by your coating manufacturer and specification.
Test on your coating
Send the coating product, its thickness and the substrate. A test on a representative sample gives the profile and end state you can write into the specification.